Dry ice is just solid carbon dioxide. At atmospheric pressure it sits at -78,5°C and sublimes directly into gas without ever becoming liquid. That's the baseline everything else builds on. When people ask for the "formula do gelo seco," they usually mean one of two things: the stoichiometric calculation for how much gaseous CO2 you need to produce a given mass of solid CO2, or the thermodynamic math behind the compression-expansion cycle that actually makes the pellets. I'll cover both because in practice you need them together.
formula do gelo seco — the core calculation
The main formula you'll use is straightforward. Take the ideal gas law rearranged for mass:
m = (P × V × M) / (R × T)
Where:
- m = mass of CO2 in kilograms
- P = absolute pressure in pascals (Pa)
- V = volume in cubic meters (m³)
- M = molar mass of CO2 = 44,01 g/mol (0,04401 kg/mol)
- R = universal gas constant = 8,314 J/(mol·K)
- T = absolute temperature in kelvin (K)
So if you have a tank at 60 bar and 20°C holding 50 liters of gas, you plug in:
P = 6.000.000 Pa
V = 0,05 m³
T = 293,15 K
m = (6.000.000 × 0,05 × 0,04401) / (8,314 × 293,15) 5,54 kg of CO2
That 5,54 kg is your theoretical maximum yield of dry ice. In reality you're looking at about 85–90% of that number once you account for valve losses, line residue, and the fact that not every molecule precipitates out cleanly during expansion.
I learned this the hard way on a job where I calculated a 10 kg batch and only got 7,2 kg out of the press. Turns out the feed line was at -20°C instead of the expected -40°C because the heat exchanger had a bad valve. Cold feed gas holds more density, and the mass flow meter was reading high while the actual mass being delivered was lower. Workaround was to install a thermocouple right at the inlet of the precipitation chamber and cross-reference the mass flow reading against the actual temperature. Once I did that, yields jumped to 9,4 kg consistently. Takes about ten minutes to set up but saves you from guessing all day.
The expansion process — what actually turns gas into solid
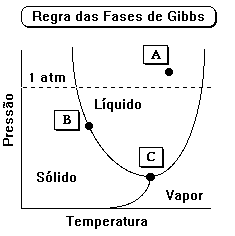
You can't just cool CO2 at atmospheric pressure and expect dry ice. The phase diagram matters here. CO2 only exists as a solid below its triple point at -56,6°C and 5,11 bar. Below that pressure, it goes straight from gas to solid (deposition). That's why dry ice makers work the way they do: they take high-pressure liquid CO2 and flash it through a nozzle into near-atmospheric pressure.
The Joule-Thomson effect does the heavy lifting. When compressed liquid CO2 passes through a restriction, it expands rapidly. Part of the fluid flash-evaporates, and that phase change pulls latent heat from the remaining fluid. The temperature drops fast — from around 20°C down to -78,5°C in milliseconds. The solid particles form in what's called CO2 snow, and then a pelletizer compresses that snow into blocks or pellets.
The energy balance for this is:
h_in = h_out + (V²_out - V²_in)/2
Where h is enthalpy. For most practical purposes you can assume the kinetic energy terms are negligible compared to the enthalpy change, which simplifies to:
h_in h_out
This is an isenthalpic expansion. You look up the inlet enthalpy on a CO2 property table, find where that same enthalpy intersects the low-pressure side, and the quality (fraction that became solid) tells you your yield.
Here's a counter-intuitive thing most beginners miss: higher inlet pressure doesn't always mean higher yield. Beyond about 70 bar, the extra pressure barely changes the outlet quality because you're already well into the two-phase region. What matters more is inlet temperature. Colder liquid CO2 going in means more solid coming out. I've seen operators run their tanks at 80 bar and get worse yields than someone running at 60 bar because the 80-bar tank hadn't been circulated and had a hot spot near the top. Stirring the liquid before drawing from it is something nobody teaches in the basic manuals but it changes everything.
Sublimation rate calculation
Once you have your dry ice, you need to know how fast it disappears. That's governed by:
dm/dt = (h × A × T) / H_sub
Where:
- dm/dt = sublimation rate (kg/s)
- h = heat transfer coefficient (W/m²·K) — roughly 5–15 for still air, higher with forced convection
- A = surface area exposed (m²)
- T = temperature difference between ambient and dry ice (-78,5°C)
- H_sub = latent heat of sublimation = 571 kJ/kg
A 5 kg block with roughly 0,3 m² of surface area in a 25°C room with still air (h 8) sublimes at about 0,014 kg/h. That's roughly one gram per minute. Put a fan on it and you're looking at triple that rate. Surface area is the variable you control. Pellets sublime faster than a solid block because they have more area for the same mass. If you need longevity, buy or make blocks. If you need rapid cooling, use pellets or flake.
Common pitfalls I see people mess up
Using the ideal gas law at high pressures without a compressibility factor. CO2 at 60 bar has a compressibility factor Z of about 0,85. Ignoring that overestimates your mass by roughly 15%. That's a real problem when you're costing out a production run. Use the Benedict-Webb-Rubin equation or just pull values from an NIST CO2 property table instead of assuming ideal behavior.
Assuming the triple point pressure is 1 atm. It isn't. It's 5,11 bar. If you're trying to make dry ice by just cooling CO2 at normal atmospheric conditions, you're relying on the flash expansion method, not simple cooling. You can't put a tank of CO2 gas in a freezer and expect snow. The pressure has to be right.
Neglecting the effect of impurities. Technical-grade CO2 often has trace moisture and oil. Moisture freezes inside your nozzles and restricts flow. I had a batch where the nozzle clogged every 40 minutes because the upstream dryer cartridge was saturated. Switching to a desiccant dryer with a dew point monitor cut the downtime to once per shift. Cost about R$2.300 in equipment but paid for itself in two weeks in saved labor and wasted CO2.
What this method doesn't handle well
The formulas above assume steady-state operation. Real presses cycle. The injection valve opens and closes, pressure waves move through the line, and the snow density varies from shot to shot. If you need precision yields — say you're producing pharmaceutical-grade dry ice for lyophilization — these rough calculations won't cut it. You need inline mass flow measurement and a closed-loop control system that adjusts valve timing based on actual snow output. The math gets a lot more complicated and you're no longer working with pen-and-paper formulas.
For small-scale or hobbyist use, the ideal gas law approach with a 10–15% deduction for real-world losses is fine. For anything commercial, invest in proper instrumentation. The formulas are the starting point, not the finish line.
Galeria
Formula Do Gelo Seco - RETOEDU
Por que o gelo-seco sublima? A sublimação do gelo-seco
FBNET | Tr20 - O diagrama de estado do GELO SECO ou dióxido de carbono ...
Fenômenos físicos e químicos / Sublimação do gelo seco. - YouTube