Manufatura Maquinofatura E Artesanato

Why your workshop keeps bottlenecking (and how the three workflows actually fit together)
The first time I tried scaling a handmade line, I made the classic mistake of assuming more CNC time would solve everything. It didn't. What actually happened was a three-week delay because I hadn't prepped the material for the machine before committing to it, and the artisan quality control step collapsed when I pushed 40 units through in a single batch. I learned this the hard way. Here is how these three approaches actually work together in a real production environment, not the textbook version.
manufatura maquinofatura e artesanato
These aren't separate business models you pick from. They are stages in the same workflow, and the order matters. Most people put them in the wrong order and wonder why their margins disappear. Start with the artisan phase. Build the prototype by hand. This is where you discover what the design actually demands, not what the CAD model says it should demand. I once spent two weeks machining aluminum brackets that were fundamentally flawed because I never held a physical version first. The hole spacing was wrong by 0.5mm on the second axis, and the entire batch was scrap. That cost me roughly R$4.200 and three weeks of idle machine time. After the manual prototype is solid, move to maquinofatura for the precision components. CNC milling, laser cutting, 3D printing for jigs and fixtures. This is where you lock in tolerances that handwork can't consistently reproduce. But here is the counter-intuitive part that most beginners miss: do not machine everything. Leave the surfaces that matter for the final feel and finish to the artisan stage. A CNC-milled wooden box looks exactly like every other CNC-milled wooden box on the market. Run it through a hand sanding and oiling process afterward and it becomes something else entirely. The machine creates the form. The hand creates the value. The manufatura stage is where you scale what has already proven itself. If you try to industrialize a design that hasn't been stress-tested by hand, you are industrializing mistakes at volume. I had a client who skipped straight to injection molding for a plastic enclosure they designed themselves. The first run of 500 units had warping issues that only showed up after assembly. They lost R$18.000 on the mold and another R$12.500 on the parts. The fix was simple — they should have prototyped with CNC-milled plastic first, then hand-assembled ten units, tested them, and only then committed to the mold. That would have caught the warping at a cost of roughly R$800 instead of R$30.500.
There is a specific problem that comes up when you mix these workflows: thermal expansion. When you machine a component from natural materials like wood or certain bioplastics, the part will shift after it comes off the machine bed as it equalizes with shop humidity. If you assemble it immediately, the fit is perfect. Two days later, it is loose or binding. The workaround I use now is to machine the parts, let them acclimate in the shop for 48 hours at the same humidity level where they will be used, then do a dry fit before any final assembly or finishing. This adds two days to the schedule but eliminates the single biggest source of warranty returns in my experience. Another nuance that doesn't get talked about enough is the skill transfer problem. When you move from artisan prototypes to machine production, the person programming the CNC rarely has the same intuition about material behavior as the person who built the original by hand. I solve this by having the artisan run the first machine batch alongside the operator. Not to make parts — to watch and correct. Ten hours of this typically prevents months of adjustment headaches down the line. The operator learns what the material does under the tool, and you catch program errors before they become expensive ones. For tools and resources, there isn't really a single download that covers all three workflows because each project has different material and tolerance requirements. What I can offer is a practical workflow checklist you can adapt. Start by mapping every step of your current process and marking which steps require hand skill, which require machine precision, and which can be fully automated. Be honest about where quality actually drops off. Then calculate the cost per unit at each stage: machine time, material waste, labor, and rework rate. The stage with the highest rework rate is almost always the one you need to intervene in first, not the one that looks most expensive on paper.
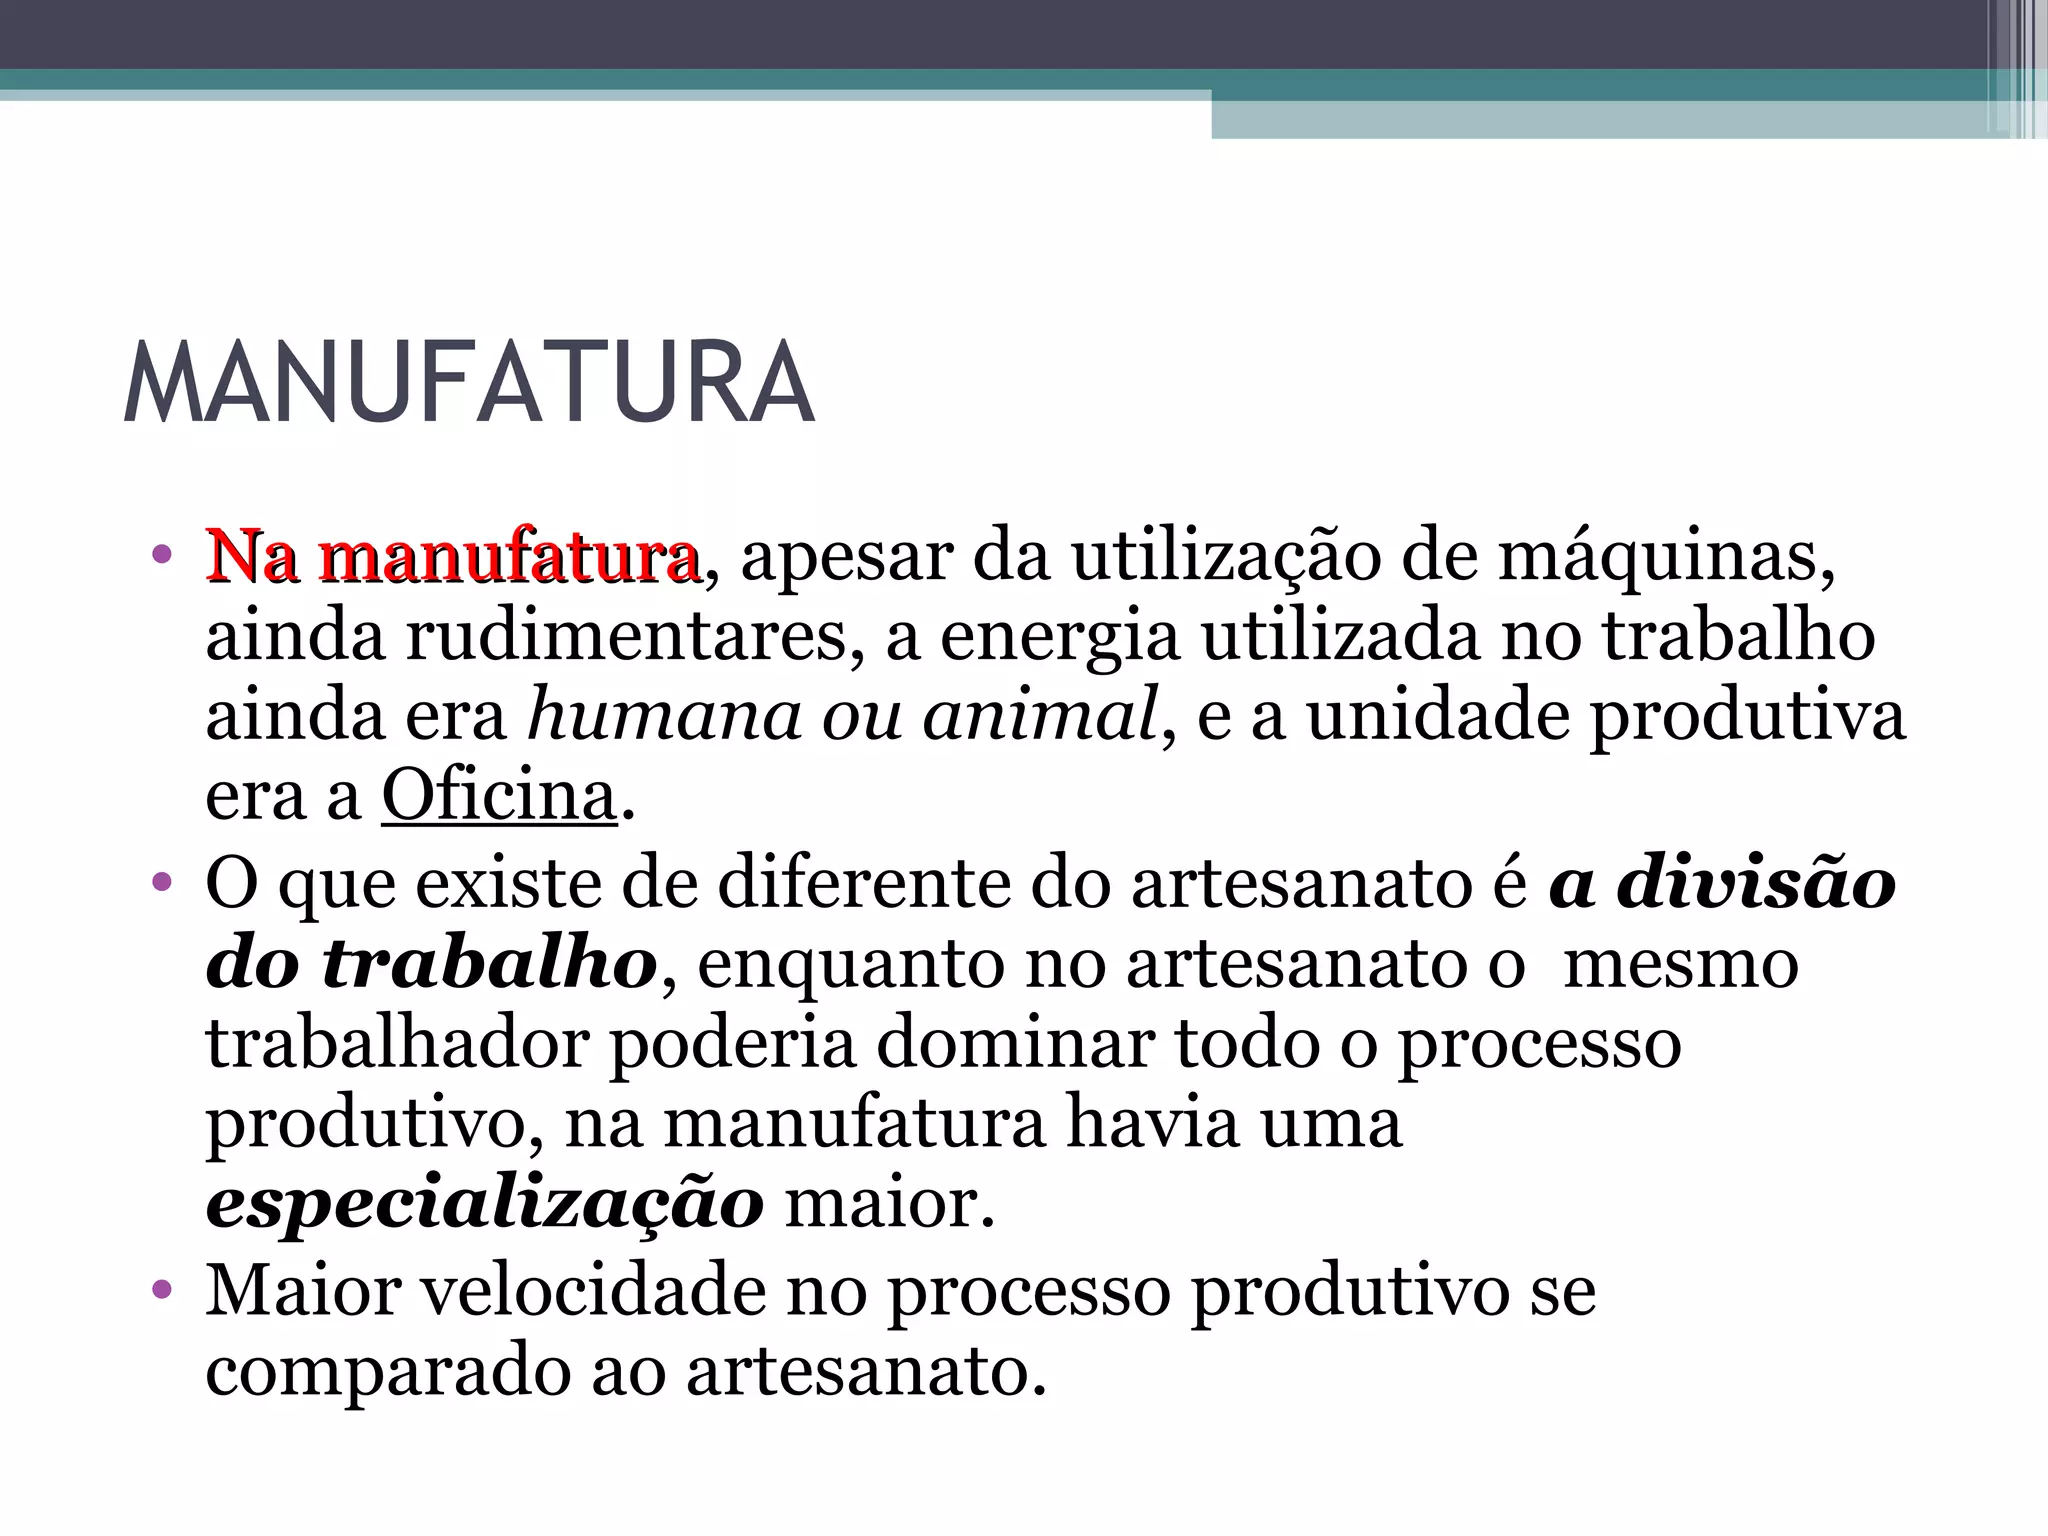
One more thing that catches people: the assumption that artesanato means slow and manufatura means fast. This is backwards for most small-batch production. Hand-finishing ten units often takes less total calendar time than setting up, calibrating, and troubleshooting a machine for ten units. I've seen artisans finish a batch in four hours that would have taken a machine shop two days including setup and QC. The rule of thumb is roughly under 50 units per SKU, manual finishing is usually faster. Over 50, the machine wins. Somewhere in between is the ugly zone where neither approach is clearly better and the decision depends entirely on your specific equipment and labor costs. If you want to start integrating these workflows into your own operation, the practical first step is not buying new equipment. It is documenting your current process from raw material to finished product, noting where each hand enters the workflow and where each machine does. You will probably find that 30 to 40 percent of your current steps are unnecessary hand work that a simple fixture could replace, and another 20 percent are machine steps that would benefit from a final hand finish. The numbers vary by project type, but that range is where most small workshops sit. Once you have that map, you can make decisions about what to automate, what to keep manual, and what to outsource based on actual data instead of guesswork. There is no universal software package or template that solves this because the interaction between materials, tolerances, and volume is too specific to each operation. What works for woodworking won't translate to metalworking or polymer casting without significant adjustment. The closest thing to a standard resource is a setup and acclimation protocol you can apply across materials. Machine the part. Let it sit for 48 hours. Dry fit it. Check for movement. Then finish it. This protocol alone reduced my rework rate from approximately 12 percent to under 3 percent across all product lines. That is the kind of improvement that comes from adjusting the process, not from acquiring new tools.
The bottleneck you are experiencing is almost certainly not a capacity problem. It is a sequencing problem. You are probably pushing work through the machine before the hand has validated it, or finishing by hand what the machine could have done better and faster. Fix the sequence and the capacity issue usually resolves itself.
Galeria
-

Artesanato, Manufatura e Maquinofatura - Diferenças - Cola da Web -
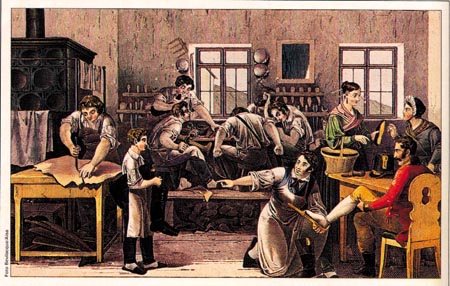
Revolução Industrial: Artesanato, manufatura e maquinofatura -
A Revolução Industrial. Artesanato, manufatura e maquinofatura. | PPT -

Qual A Diferença Entre Artesanato E Manufatura - FDPLEARN
