Qual Eletrodo Para Soldar Metalon
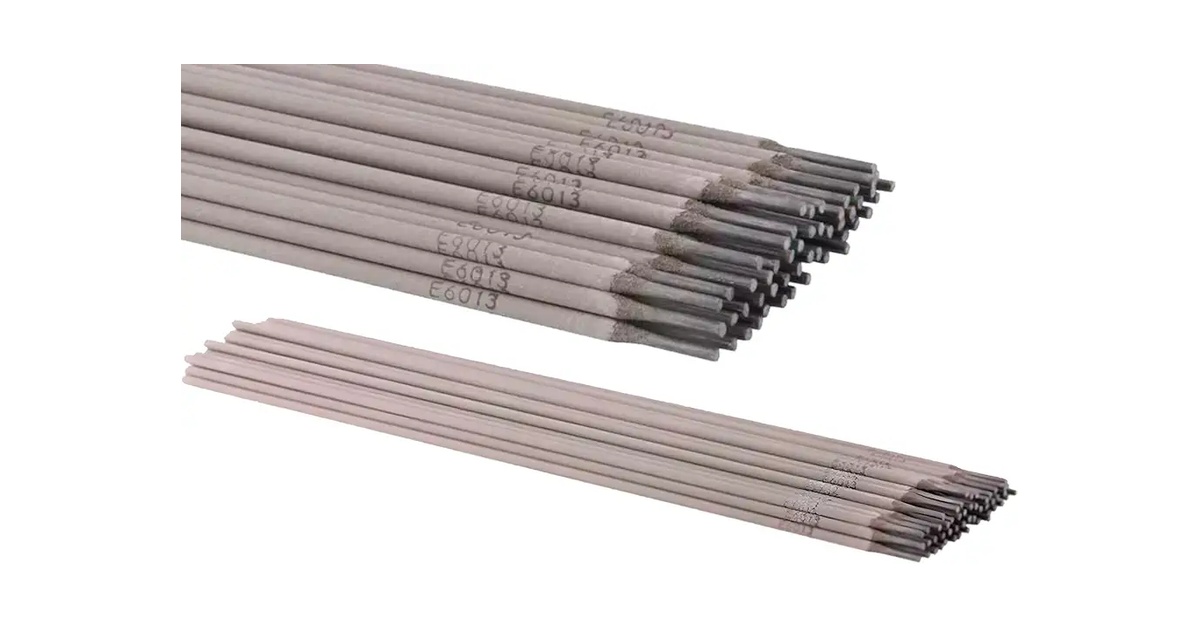
Electrodes for Welding Galvanized Steel (Metalon)
Galvanized steel is a pain to weld if you don't know what you're doing. The zinc coating boils off at around 907°C, right in the middle of your arc. You get fumes that'll make you sick, porosity in the bead, and a lot of spatter. I learned this the hard way on a site job back in 2018 where I was fitting steel frames and ignored the coating. Took me three hours to grind out defective passes because the zinc had trapped gas under the metal. So let me just lay out what actually works here, without the usual fluff you see online.
qual eletrodo para soldar metalon
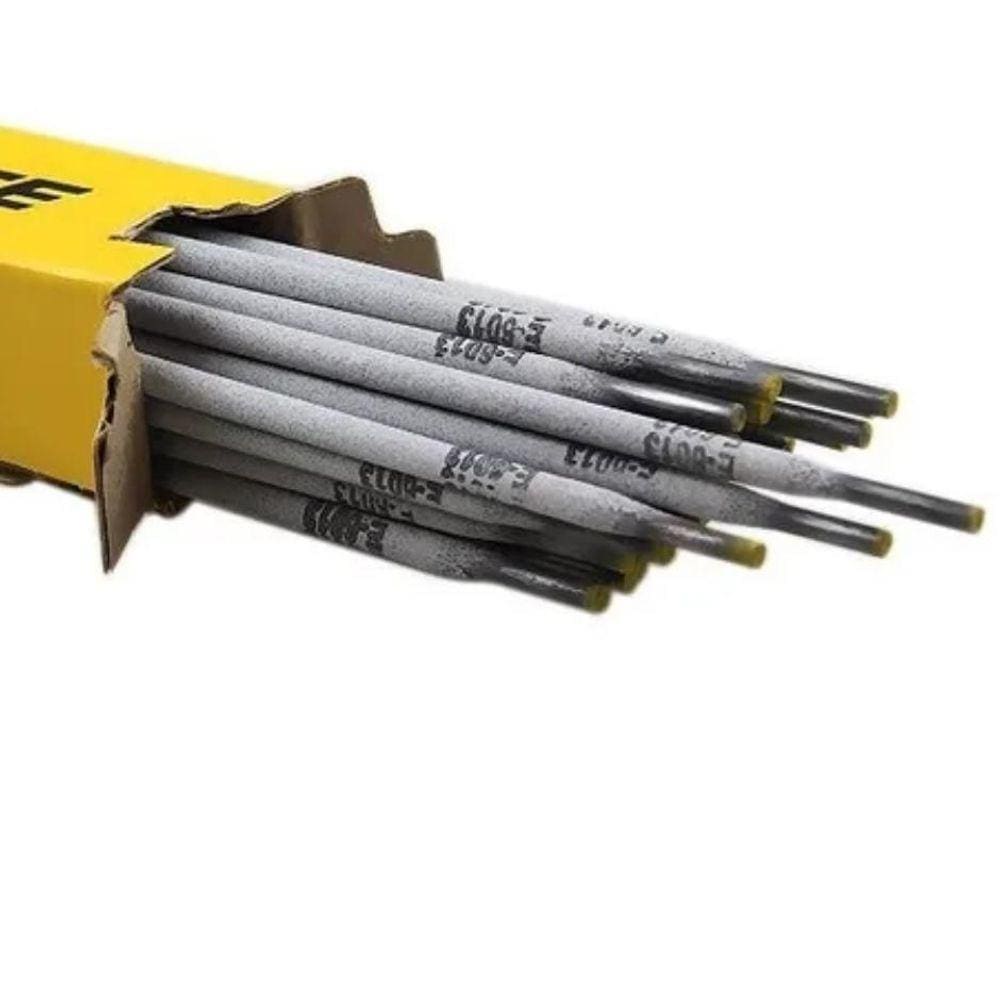
The electrode choice depends on a few things: the thickness of the material, whether you're doing repair work or fabrication, and most importantly, whether you can remove the galvanization before welding. Ideally, you should always grind or sand off the zinc coating at least 1 centimeter on each side of the weld zone. This alone cuts down fume exposure by about 80% and makes the arc significantly more stable. Now, for the electrodes themselves: Eletrodo E6013 (Rutile) — This is the most common one people reach for. It's forgiving, arcs easily even on slightly dirty surfaces, and produces a smooth bead. The downside is it doesn't penetrate as deeply, so on thicker sections of Metalon (above 3mm), you'll need multiple passes. I use this for thin-gauge fencing and light structural work. The rutile coating makes the slag easy to remove too, which saves time on cleanup.
Eletrodo E7018 (Low Hydrogen) — If you're doing structural welding on galvanized steel where strength matters, this is the better choice. The low-hydrogen formula means less risk of cracking in the heat-affected zone, which is important because the zinc residue can introduce hydrogen into the weld pool even after you've ground the coating off. The catch is it demands dry electrodes. If your E7018 has absorbed any moisture from the air, you're asking for porosity. Keep them in their original sealed container until you need them, and store the running supply in an oven at about 120°C. I've seen guys skip this step and wonder why their welds look like Swiss cheese. Eletrodo E7016 — Similar to the E7018 but with a potassium-based coating instead of sodium. It runs a bit rougher and requires AC or DC reverse polarity. I usually only recommend this if the E7018 isn't available or if you're working with equipment that only does AC. The penetration is decent and the mechanical properties are comparable, but the arc isn't as stable. It's a backup, not a first choice. There's also the Eletrodo de aço inoxidável, specifically the 308L or 309L variants, when you're welding dissimilar materials or doing repairs where corrosion resistance matters afterward. These are overkill for standard Metalon work but worth knowing about if your application calls for it.
One thing nobody talks about enough: the amperage. When welding galvanized steel, especially with E7018, running too hot is a mistake beginners make. They think more heat equals better fusion, but with the zinc layer still partially present, high amperage just throws more toxic fumes and increases spatter. Dial it back about 10-15% from what you'd use on bare steel. For a 3.25mm E7018 rod, I typically run between 90 and 110 amps on 3mm Metalon. For 4mm material, maybe 120 to 140 amps. Your millimeter-per-minute travel speed matters more than cranking up the current. ventilation is non-negotiable. Even with the coating removed, there will always be some residual zinc, and the fumes from heating galvanized steel contain zinc oxide, which causes metal fume fever. Symptoms include headache, fever, chills, and nausea, usually appearing a few hours after exposure. I've had this happen twice, once after a full day of welding without proper extraction. One job site had a portable fan blowing across the weld area — that's not ventilation, that's just spreading the fumes around. Use a proper fume extractor or at minimum position yourself so the wind is at your back, not pushing the fumes toward your face. Another practical tip: if you're doing repair work where removing the zinc coating isn't feasible, you can still weld over it with E6013 using a weaving technique. Move the rod side to side quickly across the joint. This dilutes the zinc into the weld pool rather than letting it concentrate in one spot, which reduces porosity. The bead won't be pretty, and you'll lose some tensile strength compared to clean steel, but for non-critical repairs it's acceptable. I did this on a gate repair last year where the client didn't want to pay for grinding the entire frame. The weld held for eighteen months before the surrounding zinc finally degraded from moisture exposure. That's a limitation of this approach you need to factor in.
Post-weld cleaning is another step people rush through. The slag from E7013 comes off easily with a chipping hammer and wire brush. With E7018, the slag is thinner and harder to remove, so a grinder with a flap disc works faster. Don't skip inspecting the weld before painting or recoating it. Look for cracks, excessive spatter, or areas where the zinc seems to have burned through without proper fusion underneath. If you're doing a lot of galvanized steel work regularly, consider switching to MIG welding with a gas mix of 75% argon and 25% CO2. It produces far fewer fumes because the wire feed is continuous and you can control the heat input more precisely. The initial setup cost is higher, but for production work the efficiency gain is real. I moved my team from stick to MIG for a commercial project last year and cut our welding time per joint by roughly forty percent. Here's what I'd summarize without wrapping it up neatly: use E7018 when strength and crack resistance matter, E6013 for general purpose work on thinner gauge, always grind the coating off whenever possible, keep your amperage moderate, and prioritize fume extraction over anything else. The zinc isn't going away, so work around it rather than fighting it.
Galeria
-

Qual é o Melhor Eletrodo para Soldar Metalon? Entenda! -
Qual o melhor eletrodo soldar metalon | Pontofrio -

Qual o melhor eletrodo soldar metalon | Pontofrio -

Como soldar metalon com eletrodo - YouTube | Serra fita para madeira ...
